WIRE EDM

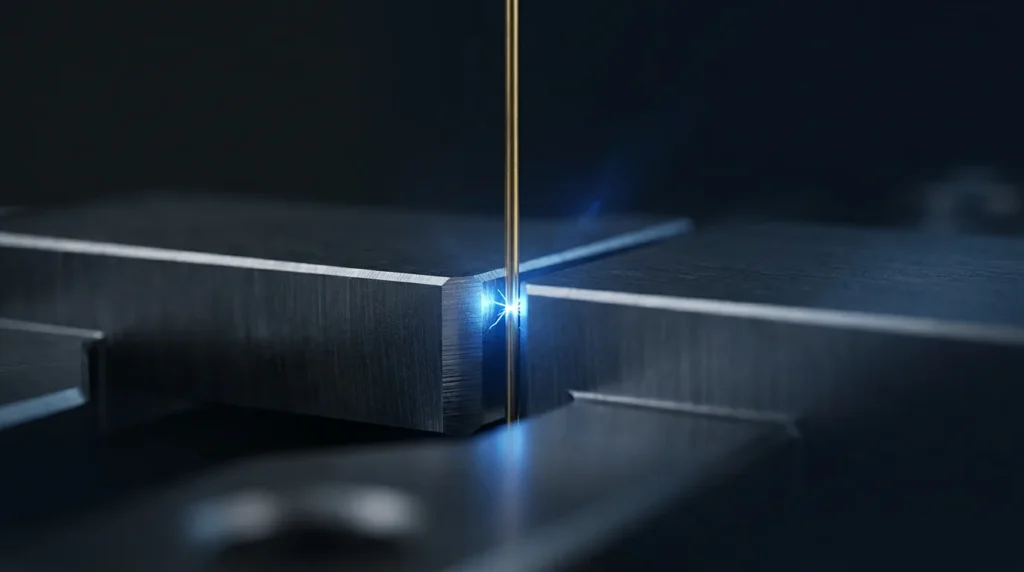
Submerged 4-axis wire EDM cutting fully hardened steel, carbide and superalloys to ± 0.0001″. No cutting force means no deflection on thin webs, and no burr means no secondary deburring operation in your routing.

CAP-01
± 0.0001"
Wire EDM brass wire cutting a hardened steel block with blue spark gap

SPECIFICATIONS

AXES4-axis, independent taper to 30°
MAX WORKPIECE23″ x 15″ x 12″, 2,200 lb
WIRE DIAMETER0.004″ – 0.012″ brass and coated
TOLERANCE± 0.0001″ positional, ± 0.0002″ contour
CORNER RADIUS0.0025″ internal minimum
SURFACE FINISHTo 16 µin Ra, skim-cut passes
MATERIAL HARDNESSUnlimited — 70+ HRC routine
LEAD TIME4–8 days standard · 2 days expedite

Materials we run

Hardened D2 / A2 / M2CarbideTi-6Al-4VInconel 718WaspaloyH13 62 HRC440CCopper tungstenMolybdenum

TYPICAL USE CASES

Stamping die details

Punches, buttons and inserts cut after heat treat — no grind-back allowance needed.

Extrusion and form tooling

Tapered profiles and precision reliefs in one submerged program.

Aerospace test coupons

Fir-tree and dovetail slots in turbine hardware with certified profile reports.

GUARANTEE

Quote within 24 hours of receiving your print. Expedite lanes ship in 3 days on qualified jobs.