SINKER EDM

Ram EDM with automatic electrode changing for cavities and details no rotating tool can reach. Sharp internal corners, deep narrow ribs and mirror finishes burned into fully hardened material.

CAP-02
± 0.0002"
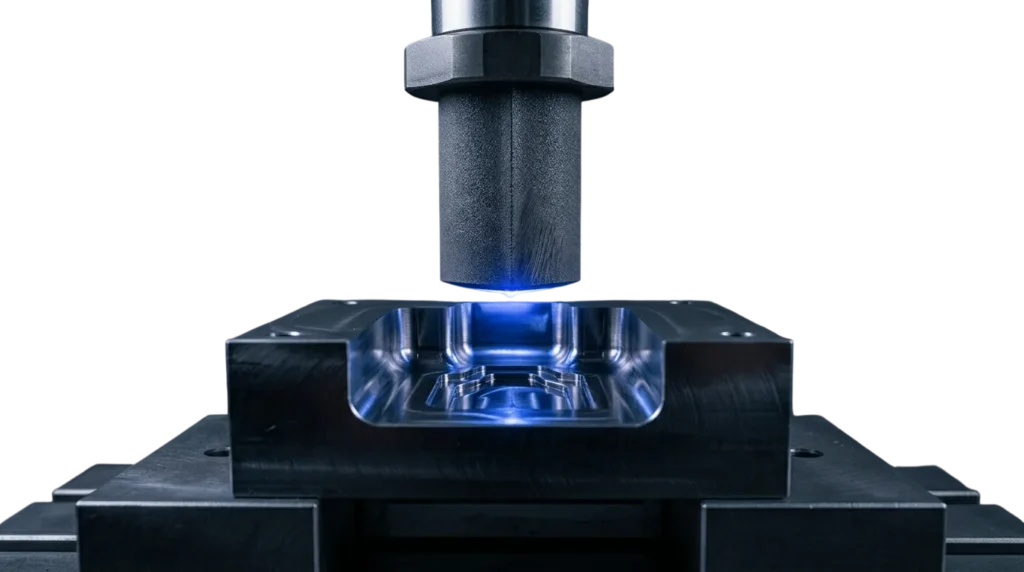
Sinker EDM graphite electrode burning a cavity into a hardened steel block

SPECIFICATIONS

AXES3-axis with orbital cycles
MAX WORKPIECE27″ x 18″ x 14″, 3,000 lb
ELECTRODESGraphite and copper, in-house ATC
TOLERANCE± 0.0002″
SURFACE FINISHTo 4 µin Ra mirror
CORNER RADIUSEffectively sharp, 0.001″ typical
LEAD TIME5–9 days standard

Materials we run

H13 / P20 / S7Hardened A2 · D2Beryllium copperInconel 718Carbide420 SSMoldmax

TYPICAL USE CASES

Injection mold cavities

Textured and polished cores with sharp corner detail.

Forging die impressions

Deep ribs in H13 at full hardness.

Keyways and internal splines

Blind features on finished shafts and hubs.

GUARANTEE

Quote within 24 hours of receiving your print. Expedite lanes ship in 3 days on qualified jobs.