AS9100DISO 9001:2015ITAR REGISTEREDDFARS COMPLIANTNADCAP

TIGHT TOLERANCE.
TIGHTER
TIMELINE.

Wire & Sinker EDM, hole-popping, advanced 3D printing and laser marking for aerospace, defense, medical and industrial programs.

Titanium, Inconel, hardened tool steel — held to ± 0.0001″ and shipped on schedule.

± 0.0001″ REPEATABLE / 70+ HRC CAPABLE / QTY 1 → 10,000

PART_NO. AX-4471-TI
WIRE EDM / TI-6AL-4V
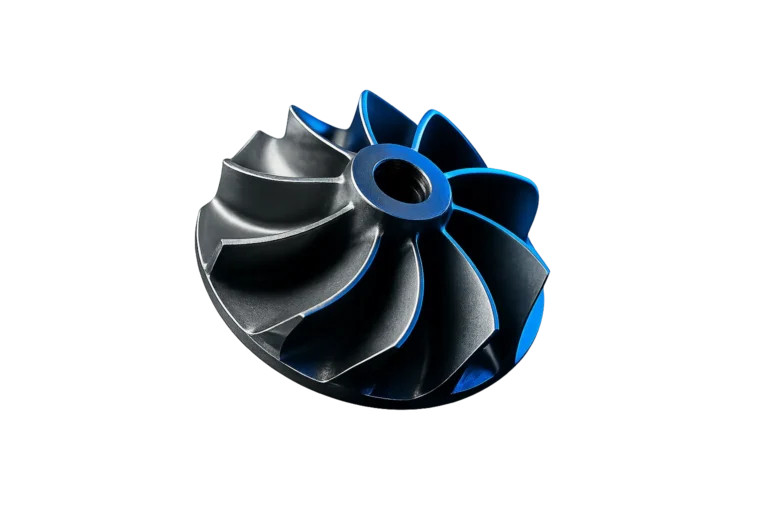
Titanium impeller with blue rim light, wire EDM cut Ti-6Al-4V

Ø 1.4870  +.0001 / -.0000

Ra 8 µin FINISH

TOLERANCE
± .0001"
HARDNESS
70 HRC
LEAD TIME
5 DAYS
ON-TIME DELIVERY, 2025
0 .6%
QUOTE TURNAROUND
0 hr
EDM & ADDITIVE MACHINES ON FLOOR
0
PARTS SHIPPED PER YEAR
0 k

STEP FILE IN. QUOTE OUT IN 24 HOURS.

02 / WHY AEROX

BUILT FOR THE PARTS OTHER SHOPS QUOTE AND THEN DECLINE

01

Hardness is not a constraint

Wire and sinker EDM cut at 70+ HRC, so your part gets heat treated before finishing instead of fighting for size after.

02

Five processes, no outside vendors

EDM, additive and marking happen under one roof and one quality plan. Nothing in your critical path sits on a courier.

03

Metrology that proves it

CMM and vision inspection with first-article reports, GD&T layouts and material certs shipped with every lot.

04

Expedite capacity held back on purpose

We reserve daily machine hours for rush work rather than promising three days and then backfilling the schedule.

CERTIFIED & COMPLIANT
AS9100DISO 9001:2015ITAR REGISTEREDDFARS 252.204-7012NADCAP PROCESSING
03 / PROCESS

PRINT TO PACKING SLIP

STEP 01

Send the print

STEP, IGES or PDF with quantity and need-by date. ITAR data accepted.

STEP 02

Engineering review

DFM feedback on features that will cost you money before anyone quotes.

STEP 03

Firm quote in 24 hrs

Price, process routing and a committed ship date — not a range.

STEP 04

Cut and inspect

In-process gauging with CMM first-article before the run continues.

STEP 05

Ship with paper

FAI report, material certs and CoC in the box. Marking done in-house.

04 / APPLICATIONS

WHERE OUR PARTS END UP

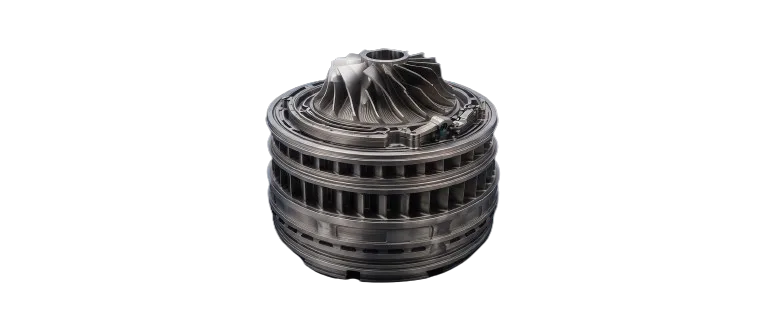
Turbine stage assembly for aerospace, EDM-machined components

Aerospace

Structural fittings, actuation hardware and turbine details under AS9100D.

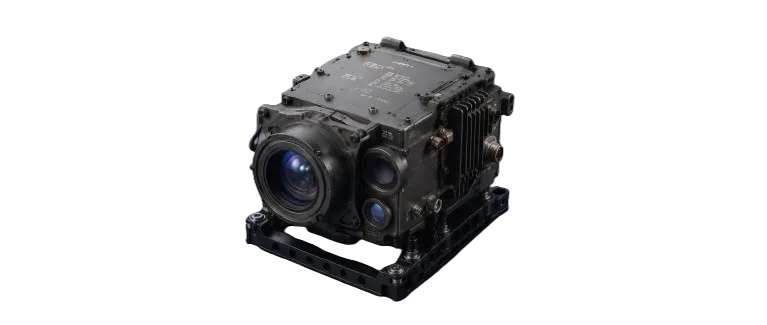
Military optics housing for defense programs, ITAR-controlled hardware

Defense

ITAR-controlled assemblies, optics mounts and ordnance components.

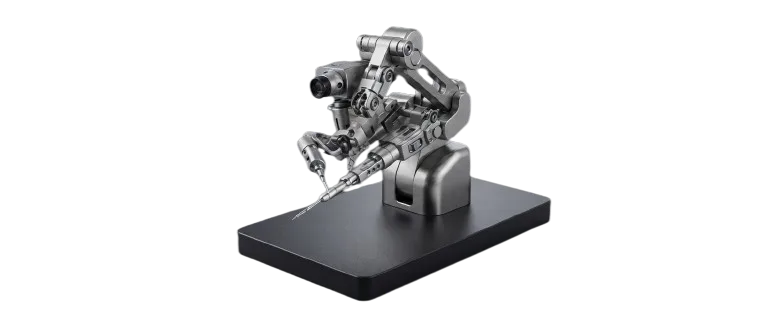
Surgical robotic instrument arm on base, medical device components

Medical

Instrument bodies and implant-adjacent parts with UDI marking.

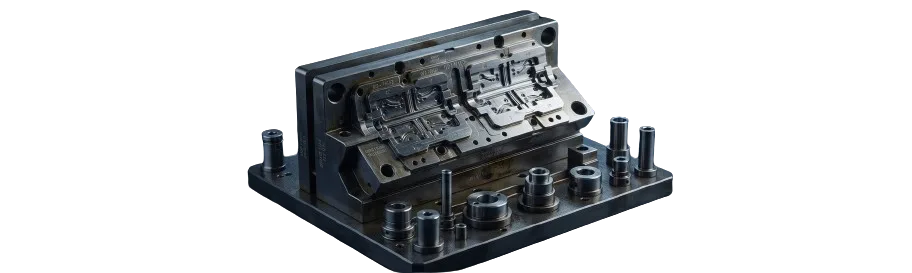
Hardened stamping die insert with fixturing bolts, industrial tooling

Industrial

Die details, extrusion tooling and production fixtures in hardened steel.

05 / FAQ

QUESTIONS WE GET DAILY

Within 24 hours of receiving a print or STEP file, guaranteed. Send quantity, material and required date and the quote comes back from the engineer who would program the job.

± 0.0002″ is routine across sinker EDM and additive work, and ± 0.0001″ is repeatable on wire EDM. Anything tighter, we will tell you up front what the process capability is instead of quoting and hoping.

Yes. Wire and sinker EDM cut at any hardness, including 70+ HRC tool steel and carbide, so parts can be hardened before finishing rather than after.

AS9100D and ISO 9001:2015 certified, ITAR registered and DFARS compliant. Certificates and our quality manual are available on request.