HOLE-POPPING EDM

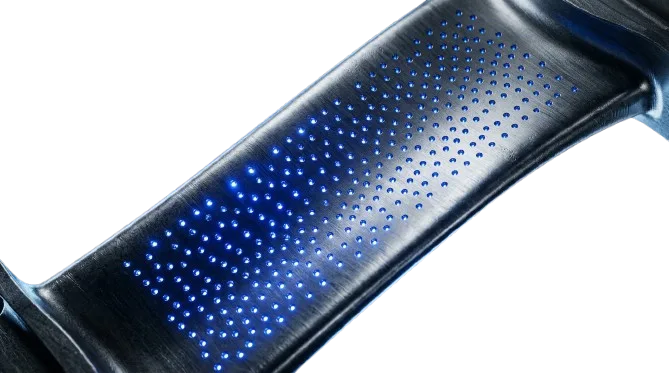
High-speed EDM drilling of holes from 0.004″ diameter at aspect ratios past 200:1 — cooling passages, weep holes, wire start holes and broken tap removal without damaging the surrounding part.

CAP-03
± 0.0005"
Array of small EDM-drilled cooling holes in a curved metal blade

SPECIFICATIONS

HOLE DIAMETER0.004″ – 0.250″
DEPTH RATIOUp to 200:1
MAX DEPTH16″
TOLERANCE± 0.0005″ diameter and position
ANGLED ENTRYCompound angles to 45° on curved surfaces
LEAD TIME2–5 days · same-day rescue jobs

Materials we run

Inconel 718 / 625Ti-6Al-4VHastelloyHardened tool steelCarbideStainlessBroken taps and drills in customer parts

TYPICAL USE CASES

Turbine cooling holes

Patterned arrays at compound angles with position reports.

Wire EDM start holes

Feeding downstream wire work on closed contours.

Broken tool rescue

Removing snapped taps from high-value castings without scrapping them.

GUARANTEE

Quote within 24 hours of receiving your print. Expedite lanes ship in 3 days on qualified jobs.